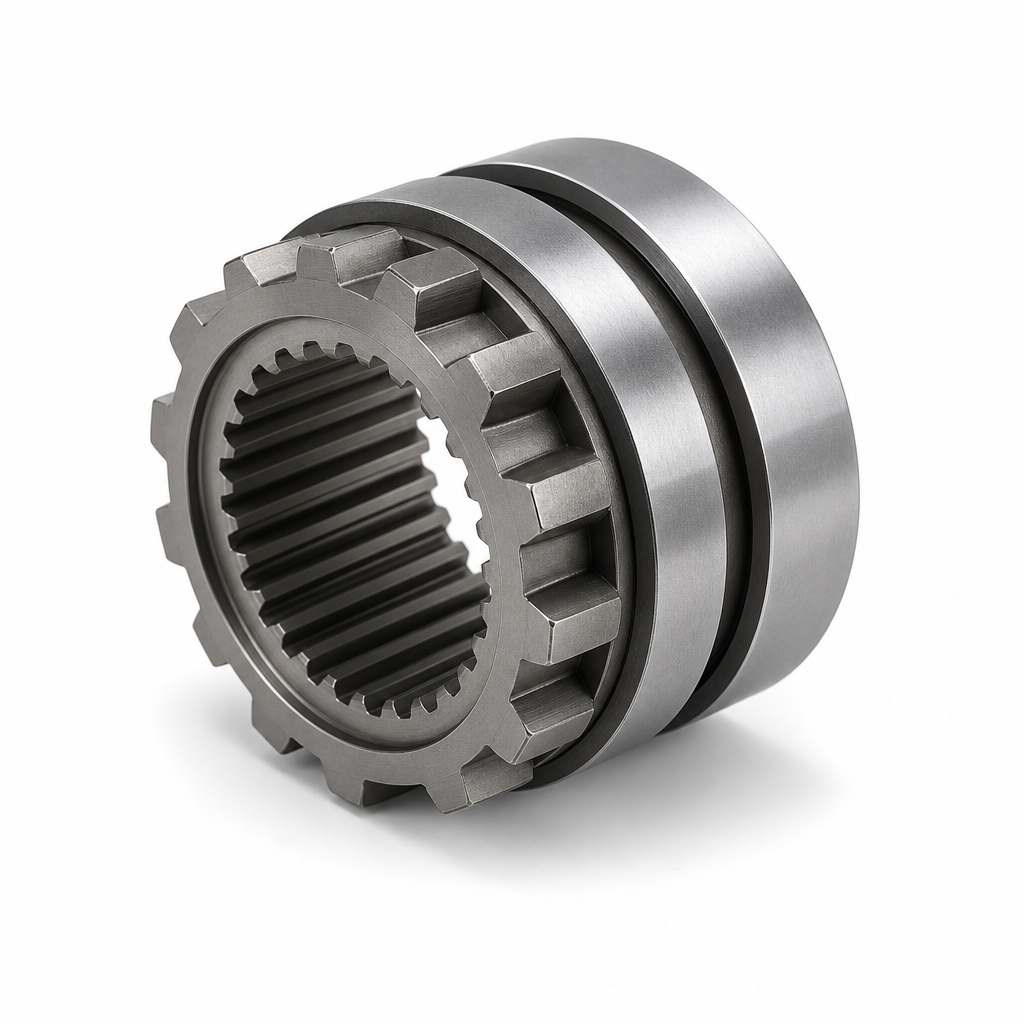
A clutch sleeve with dog teeth on the outside and an involute spline inside, both cut from the same datum, with the face chamfer acting as the lead-in. This is the steel part we build most for gearbox and PTO customers.
The acceptance points here are not on the outline. There are two: the relative phase between the internal spline and the external teeth, and what carburizing does to the internal spline. Let the phase drift and the teeth butt against each other on engagement instead of sliding in; let the spline distort in the quench and the part will not go on the shaft. So the external teeth are hobbed or shaped against the same datum as the spline, phase is held to ±0.05 mm, case depth runs 0.6–0.9 mm at 58–62 HRC, and the internal spline is ground after hardening. The face chamfer stays at 15°–20° as the lead-in.
Send the tooth count, module or diametral pitch, spline standard (DIN 5480, ANSI B92.1 or GB/T 3478), torque and shift type. We will confirm the heat treatment route — carburize or Q&T plus induction — and the grinding allowance, then quote with hardness, case depth and tooth inspection reports. Reply within 48 hours.