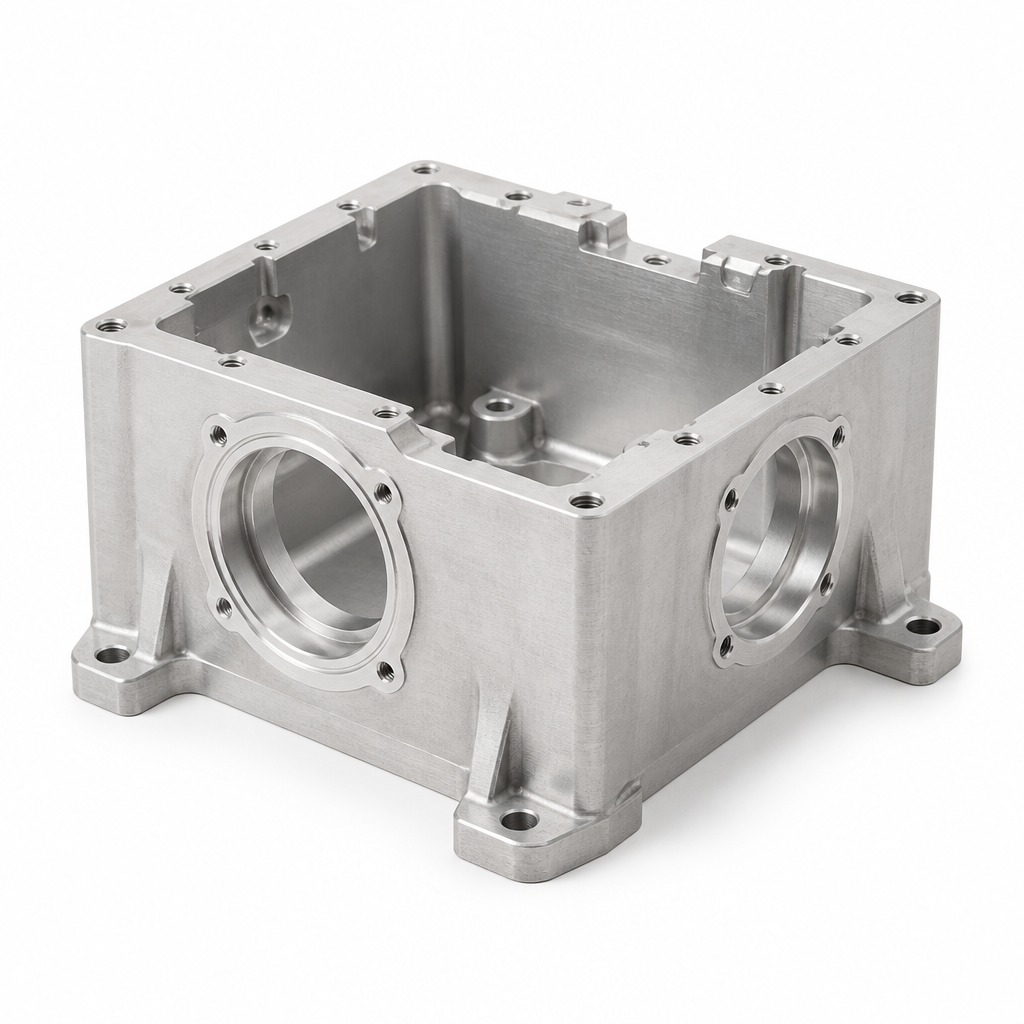
The bearing bores on the two opposite walls must be coaxial: they are line-bored in one setup before the top joint face is cut, which keeps the bore axis parallel to that face.
The four feet are left with stock so they can be spot-faced to the actual machine frame at assembly.