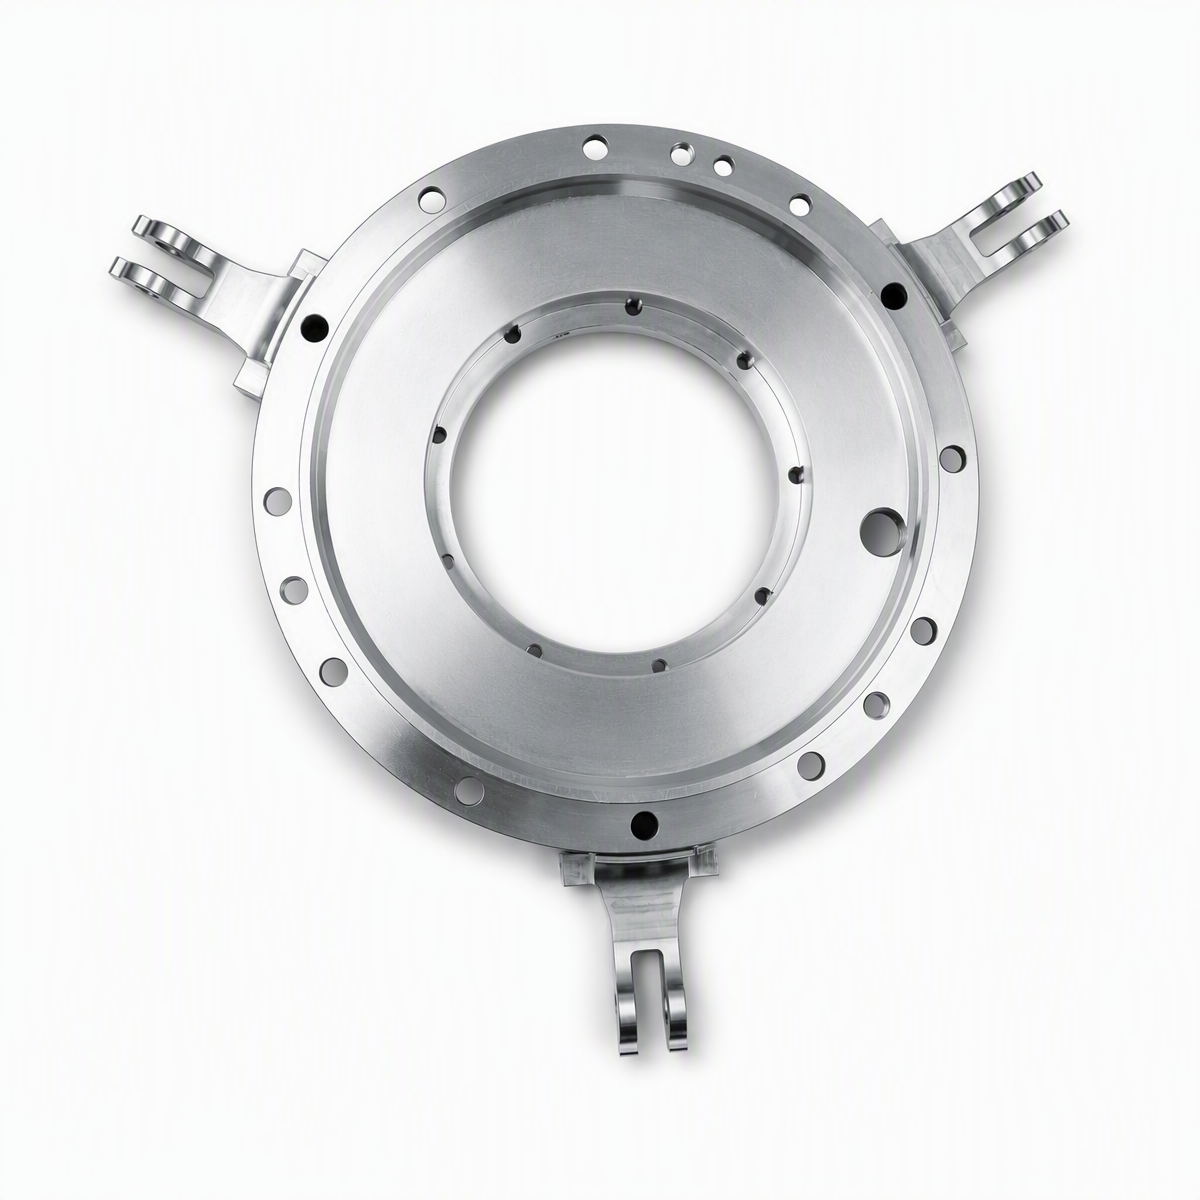
A three-lug mounting ring where the outer bolt circle, the inner connection holes and the three clevis lugs are located from one datum. This is the ring pattern we build most for automation equipment, hydraulic actuator and rotary table customers.
Two things make this part hard: a thin wall that loses its roundness, and the angular position of the lugs. On a Ø400-class ring a slightly heavy chuck jaw turns the part oval, so it is roughed, released and stress-relieved, then finished on a fixture that clamps evenly — that is how roundness holds at 0.02 mm. The three lugs sit at 120° with ±0.1° angular position, and the pin bores are H7, concentric to the main bore within Ø0.05 mm, so the actuator bolts up without binding and the pins actually go in.
Send the outer diameter, bore fit, lug count and angle, pin bore size and pin specification — or just the assembly drawing. We will confirm the blank form (rolled ring or plate cut), the number of stress-relief cycles and the fixturing, then quote with CMM, roundness and lug position reports. Reply within 48 hours.